How to Choose Blister Thermoforming Machines in 2026?

Choosing a blister thermoforming machine in 2026 requires more than comparing heating zones and advertised cycle speeds. The right decision connects product geometry, material behavior, validation needs, labor availability, and total ownership cost. A machine that forms shallow PVC pockets may struggle with deeper aluminum-based structures or sensitive medical components. Small details matter, including web width, forming temperature stability, cavity depth, sealing pressure, and changeover time.

Industry data supports a careful approach. PMMI’s recent pharmaceutical and medical packaging research highlights continuing investment in automation, flexibility, traceability, and workforce efficiency. Grand View Research’s Blister Packaging Market Size, Share and Trends Analysis reports also identify pharmaceutical demand, material development, and sustainable packaging as important market drivers. These reports show direction, not a guaranteed result. Conditions vary by region, product type, and supplier capability.

In practice, buyers should test real forming materials before approving a machine. Ask for documented trials using the intended foil, polymer, or recyclable structure. Measure scrap rates, temperature recovery, seal consistency, and operator workload. Review data logging, safety systems, spare-parts support, and validation documentation against applicable quality requirements, including ISO 11607 where medical-device packaging applies. Do not trust speed alone. Faster can mean more waste. A cheaper machine can become expensive after repeated tooling changes, unstable forming, or long service delays. The best choice may not look impressive during a showroom demonstration. It should perform reliably on an ordinary production shift, with ordinary operators, and realistic maintenance limits. That assumption deserves testing.
How to Choose Blister Thermoforming Machines in 2026?

Define Pack Requirements: PVC/PVdC, PET, Aluminum, and ISO 15223-1

Choosing a blister thermoforming machine starts with the pack, not the machine catalogue. PVC offers stable forming and low cost, while PVdC adds a moisture barrier for sensitive medicines. PET suits transparency and lower-chlorine designs. Aluminum cold-forming provides excellent light and moisture protection, but it needs different tooling and pressure control.

Smithers’ 2024 packaging outlook forecasts the global packaging market will exceed 1.3 trillion US dollars by 2029. That scale increases pressure for material efficiency and repeatable production. Ask for measured scrap rates, not only brochure claims. A recent PMMI industry report also identifies changeover speed, automation, and quality inspection as major investment priorities. These factors matter when switching between PVC, PET, and aluminum structures.

ISO 15223-1:2021 defines standardized symbols for medical device information. The machine must support accurate printing, vision checks, and readable placement without damaging the lidding foil. Test symbol contrast after sealing, not before. Forming depth, web width, heating zones, sealing temperature, and cleanroom controls should match the validated pack design. I would challenge any supplier promising one universal setup. It may work during a demonstration, then drift during a twelve-hour run. Small gaps, weak seals, or blurred symbols can become expensive quality events.

How to Choose Blister Thermoforming Machines in 2026? Start by defining the forming material, nominal thickness, sealing method, and artwork or symbol-inspection requirements.

PVC and PET are commonly thermoformed sheet materials. Aluminum blister foil is typically cold-formed rather than heated like plastic, so it requires dedicated forming and sealing capabilities. ISO 15223-1 defines medical-device symbols; it affects artwork control, print registration, and inspection rather than the forming temperature.

The chart shows representative commercial starting ranges for blister-pack materials. Actual specifications depend on the cavity design, barrier requirements, forming depth, and material supplier.

Set Output Targets: Compare 20–60 Cycles per Minute and OEE

How to Choose Blister Thermoforming Machines in 2026?

Set output targets before comparing machine specifications. A machine rated at 60 cycles per minute may not deliver 60 good cycles continuously. Cycle speed measures indexing frequency, not sellable output. Confirm cavity count, material width, forming depth, and product spacing. Run the math.

For example, 40 cycles per minute over an eight-hour shift equals 19,200 theoretical cycles. With 80% OEE, the realistic figure falls to 15,360 good cycles. If each cycle produces six blisters, that equals 92,160 acceptable packs.

This calculation prevents an expensive mismatch between machine capacity and daily demand. It also reveals whether a 20-cycle machine could meet your needs with lower energy use and simpler maintenance.

OEE combines availability, performance, and quality. Track heating delays, tool changes, web breaks, rejected seals, and short stoppages during factory trials. A practical target may be 75–85% OEE after stabilization, rather than an optimistic figure from a demonstration.

Machines operating near 60 cycles per minute need consistent temperature control, accurate indexing, and reliable scrap removal. Faster is not always better.

I have seen output targets fail because operators needed extra time for cleaning and tooling adjustments. That weakness should remain visible in your evaluation. Request shift-based data, not only peak-speed claims, and test your actual forming material before committing.

Select Forming Technology: Plate or Roller Systems for ±0.1 mm Accuracy

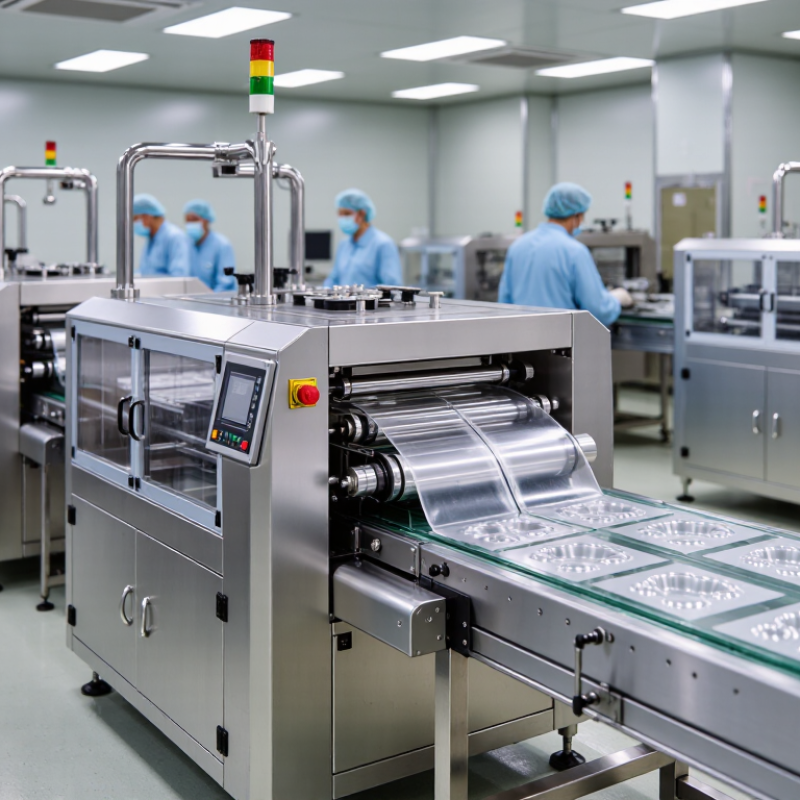
Choosing a blister thermoforming machine in 2026 starts with the forming method, not the brochure’s speed claim. Plate systems use an intermittent cycle, placing each sheet under controlled heat and pressure. This layout supports accurate cavities, stable indexing, and frequent tooling changes. Roller systems form continuously, which can increase output and reduce movement between stations. However, web tension, roller alignment, and material stretch can affect registration.

For ±0.1 mm accuracy, inspect the whole process. Ask for measured samples, not only stated specifications. Check heating-zone control, servo positioning, cooling stability, and the repeatability of cutting tools. Plate systems may hold tight dimensions more easily during short runs or complex formats. Roller systems can achieve similar precision when tension control and automatic registration work consistently. The material also matters. Different thicknesses and heat responses can change cavity depth.

I have seen accurate forming fail after a poorly controlled tooling change. Small temperature differences left visible wall variation. That mistake was not dramatic, but it reduced packing consistency. Build a trial protocol with repeated measurements across the sheet, including the first and last cycles. Record cavity length, width, depth, and seal alignment. Leave room for doubt. A machine that reaches ±0.1 mm once may not maintain it after long production, cleaning, or seasonal temperature changes. Ask how calibration is verified, how wear is detected, and whether operators can adjust settings without losing traceability.

How to Choose Blister Thermoforming Machines in 2026? - Select Forming Technology: Plate or Roller Systems for ±0.1 mm Accuracy

Typical engineering comparison for pharmaceutical, medical, electronics, and consumer-product blister packaging

Selection Dimension Plate Forming System Roller Forming System Practical Selection Guidance
Forming principle A heated sheet is indexed into a forming station and shaped against a fixed plate or mold. A continuously moving web is formed around a rotating perforated or vacuum-assisted forming roller. Select according to required indexing behavior, package geometry, and production speed.
Typical production mode Intermittent motion Suitable for batch production and frequent format changes. Continuous motion Suitable for stable, high-volume production with long runs. Plate systems generally offer greater flexibility; roller systems generally offer higher throughput.
Typical forming accuracy Approximately ±0.05 to ±0.10 mm Achievable with controlled temperature, tooling, web tension, and registration. Approximately ±0.08 to ±0.15 mm Accuracy depends strongly on roller balance, web tension, and thermal stability. For a guaranteed ±0.1 mm requirement, validate the complete process using the actual material and tooling.
Best fit for ±0.1 mm registration Strong fit for tight cavity-to-print or cavity-to-cut registration because the web stops during forming. Possible with closed-loop registration and stable continuous-web control, but more sensitive to tension variation. Choose plate forming when registration tolerance is critical and product formats change frequently.
Typical output range Approximately 15–45 cycles per minute Actual output depends on cavity count, heating time, and material thickness. Approximately 30–100+ cycles per minute Actual output depends on roller diameter, web width, product pitch, and cooling capacity. Roller systems are normally favored for high-volume, standardized products.
Common web-width range Approximately 100–600 mm Wider configurations are possible with suitable frame and heating capacity. Approximately 150–700 mm The usable width depends on roller construction and line layout. Match the usable forming width to the package nest layout and required material utilization.
Suitable forming materials PVC, PET, PETG, PP, PLA, and selected multilayer barrier films. PVC, PET, PETG, PP, and other films that maintain stable behavior during continuous forming. Confirm forming temperature, shrinkage, stiffness, and sealing compatibility for every film structure.
Typical package depth Approximately 3–35 mm, depending on material, draw ratio, cavity shape, and mold design. Approximately 3–25 mm for many continuous roller applications. Deep or irregular cavities usually provide more tooling flexibility on a plate system.
Format changeover Approximately 20–60 minutes with quick-change tooling and preheated replacement tools. Approximately 45–120 minutes because the forming roller and associated components may require replacement. Plate forming is usually more efficient for products with frequent SKU changes.
Tooling cost and complexity Generally lower initial tooling complexity; individual cavity plates can be exchanged or modified. Generally higher tooling complexity because the forming pattern is integrated into a precision roller. Roller tooling becomes more economical when the same format runs continuously at high volume.
Temperature-control requirements Zone-based heater control with mold cooling; easier to isolate heating and cooling problems by station. Precise continuous heating and roller-temperature control are required to minimize web deformation. Both systems require stable material temperature; roller systems typically demand tighter continuous control.
Web-tension sensitivity Moderate; the indexed web can reduce tension-related pitch errors during the forming step. High; tension changes can affect pitch, cavity position, wall thickness, and registration. Use automatic tension control and edge guiding when choosing a continuous roller line.
Maintenance profile Regular inspection of guide rails, vacuum circuits, heaters, molds, and indexing mechanisms. Regular inspection of roller surfaces, bearings, vacuum passages, drive synchronization, and web guides. Plate systems are generally easier to service; roller systems may require more specialized tooling maintenance.
Space and line integration Often easier to integrate with intermittent sealing, punching, vision inspection, and robotic loading. Well suited to synchronized continuous sealing, punching, printing, and high-speed downstream equipment. Select the system that matches the motion profile of the existing packaging line.
Recommended application profile Flexible production Multiple SKUs, frequent changeovers, deep or complex cavities, and tight registration. High-volume production Long production runs, stable product geometry, high output, and low changeover frequency. Base the decision on total cost per pack, not only the machine purchase price.
Primary risk to ±0.1 mm performance Indexing backlash, mold wear, uneven heating, inaccurate cut marks, and insufficient cooling. Roller eccentricity, web-tension fluctuation, thermal expansion, drive synchronization, and material shrinkage. Require a documented acceptance test using dimensional capability data from production samples.
Overall selection recommendation Preferred for precision flexibility Especially when ±0.1 mm registration and frequent product changes are priorities. Preferred for continuous efficiency Especially when output, stable formats, and long operating runs are priorities. Confirm accuracy, output, scrap rate, changeover time, and energy consumption through a production trial.

Technical note: The values shown are typical engineering ranges rather than universal machine guarantees. Actual ±0.1 mm performance depends on film properties, tooling precision, heating uniformity, vacuum or compressed-air stability, web tension, registration controls, cooling, and measurement conditions. Request a documented capability study based on the intended product and material before final selection.

Validate Seals and Materials Under ISO 11607-1 and ASTM F88/F88M

How to Choose Blister Thermoforming Machines in 2026?

A suitable blister thermoforming machine must support more than attractive cavities. It must produce stable seals across real packaging materials and operating conditions. ISO 11607-1 requires packaging systems to maintain sterility until use. Therefore, evaluate forming accuracy, sealing control, material handling, and repeatability together. Ask for recorded temperature, pressure, and dwell-time data from production-equivalent trials.

ASTM F88/F88M measures the seal strength of flexible barrier materials. It does not prove complete package integrity by itself. Prepare sealed samples using the intended blister material, lidding structure, and machine settings. Then test peel force, seal width, failure mode, and variability. A clean peel is not always a good result. Cohesive failure, adhesive separation, or film tearing can reveal different process problems.

Look closely at the machine’s adjustment range. Narrow settings may work during a short demonstration but fail after tooling changes or material lots vary. Check cavity depth, heating uniformity, cooling control, and sealing pressure at multiple positions. Keep samples from the beginning, middle, and end of each run. Small details matter.

One practical mistake is trusting average seal strength alone. The weakest result often matters more. Review conditioning, test speed, sample width, and operator technique under ASTM F88/F88M.

Document every deviation, even an inconvenient one. Validation is rarely perfect on the first attempt. That is useful information, not failure.

Audit 2026 Total Cost: Energy, Changeovers, Automation, and 21 CFR Part 11

Choosing a blister thermoforming machine in 2026 requires a total-cost audit, not a purchase-price comparison. The U.S. Department of Energy reports that motor-driven systems consume more than half of industrial electricity. Measure kilowatt-hours per thousand good packs, not only installed power. Heating zones, vacuum pumps, compressed air, and idle time can quietly inflate energy costs.

Changeovers deserve equal attention. Record the minutes from the last accepted pack to the first validated pack. Include tooling swaps, recipe loading, cleaning, and rejected startup material. A 20-minute saving repeated six times daily can outweigh a modest equipment-price difference. Yet faster is not always better. I would question any supplier claim based only on ideal factory trials. Measure it with your operators and real tooling.

Automation can reduce labor exposure, but it adds software, training, and validation work. The 2024 MHI Annual Industry Report found that 55% of surveyed supply-chain leaders planned to increase automation investment. For regulated production, confirm electronic records, audit trails, user permissions, backups, and electronic signatures. FDA guidance explains that 21 CFR Part 11 controls apply when electronic records and signatures are used in regulated activities. Keep energy, changeover, rejection, and maintenance data traceable. A machine may pass a demonstration and still fail an audit. That uncomfortable gap deserves a line in the budget.

Click to access the login or register cheese
Scroll to Top

Request a Quote

Call 815-281-5297 now to speak directly with an Algus expert or fill out the form below.